
Every time a part gets removed from a machine and repositioned for the next operation, there’s a small opportunity for error to creep in. For components with tight tolerances and intricate geometry, that repeated handling adds up fast.
The Problem With Multiple Setups
Traditional machining often requires a part to be moved between different machines or repositioned several times to complete all the necessary cuts, drilled holes, and features.
Each repositioning introduces the possibility of slight misalignment, and even a small deviation can compound across several setups until a part no longer meets spec.
Beyond the precision risk, multiple setups also add time — both in the physical repositioning and in the inspection steps typically needed to confirm each new setup is correctly aligned before cutting resumes.
What Multi-Axis Machining Changes
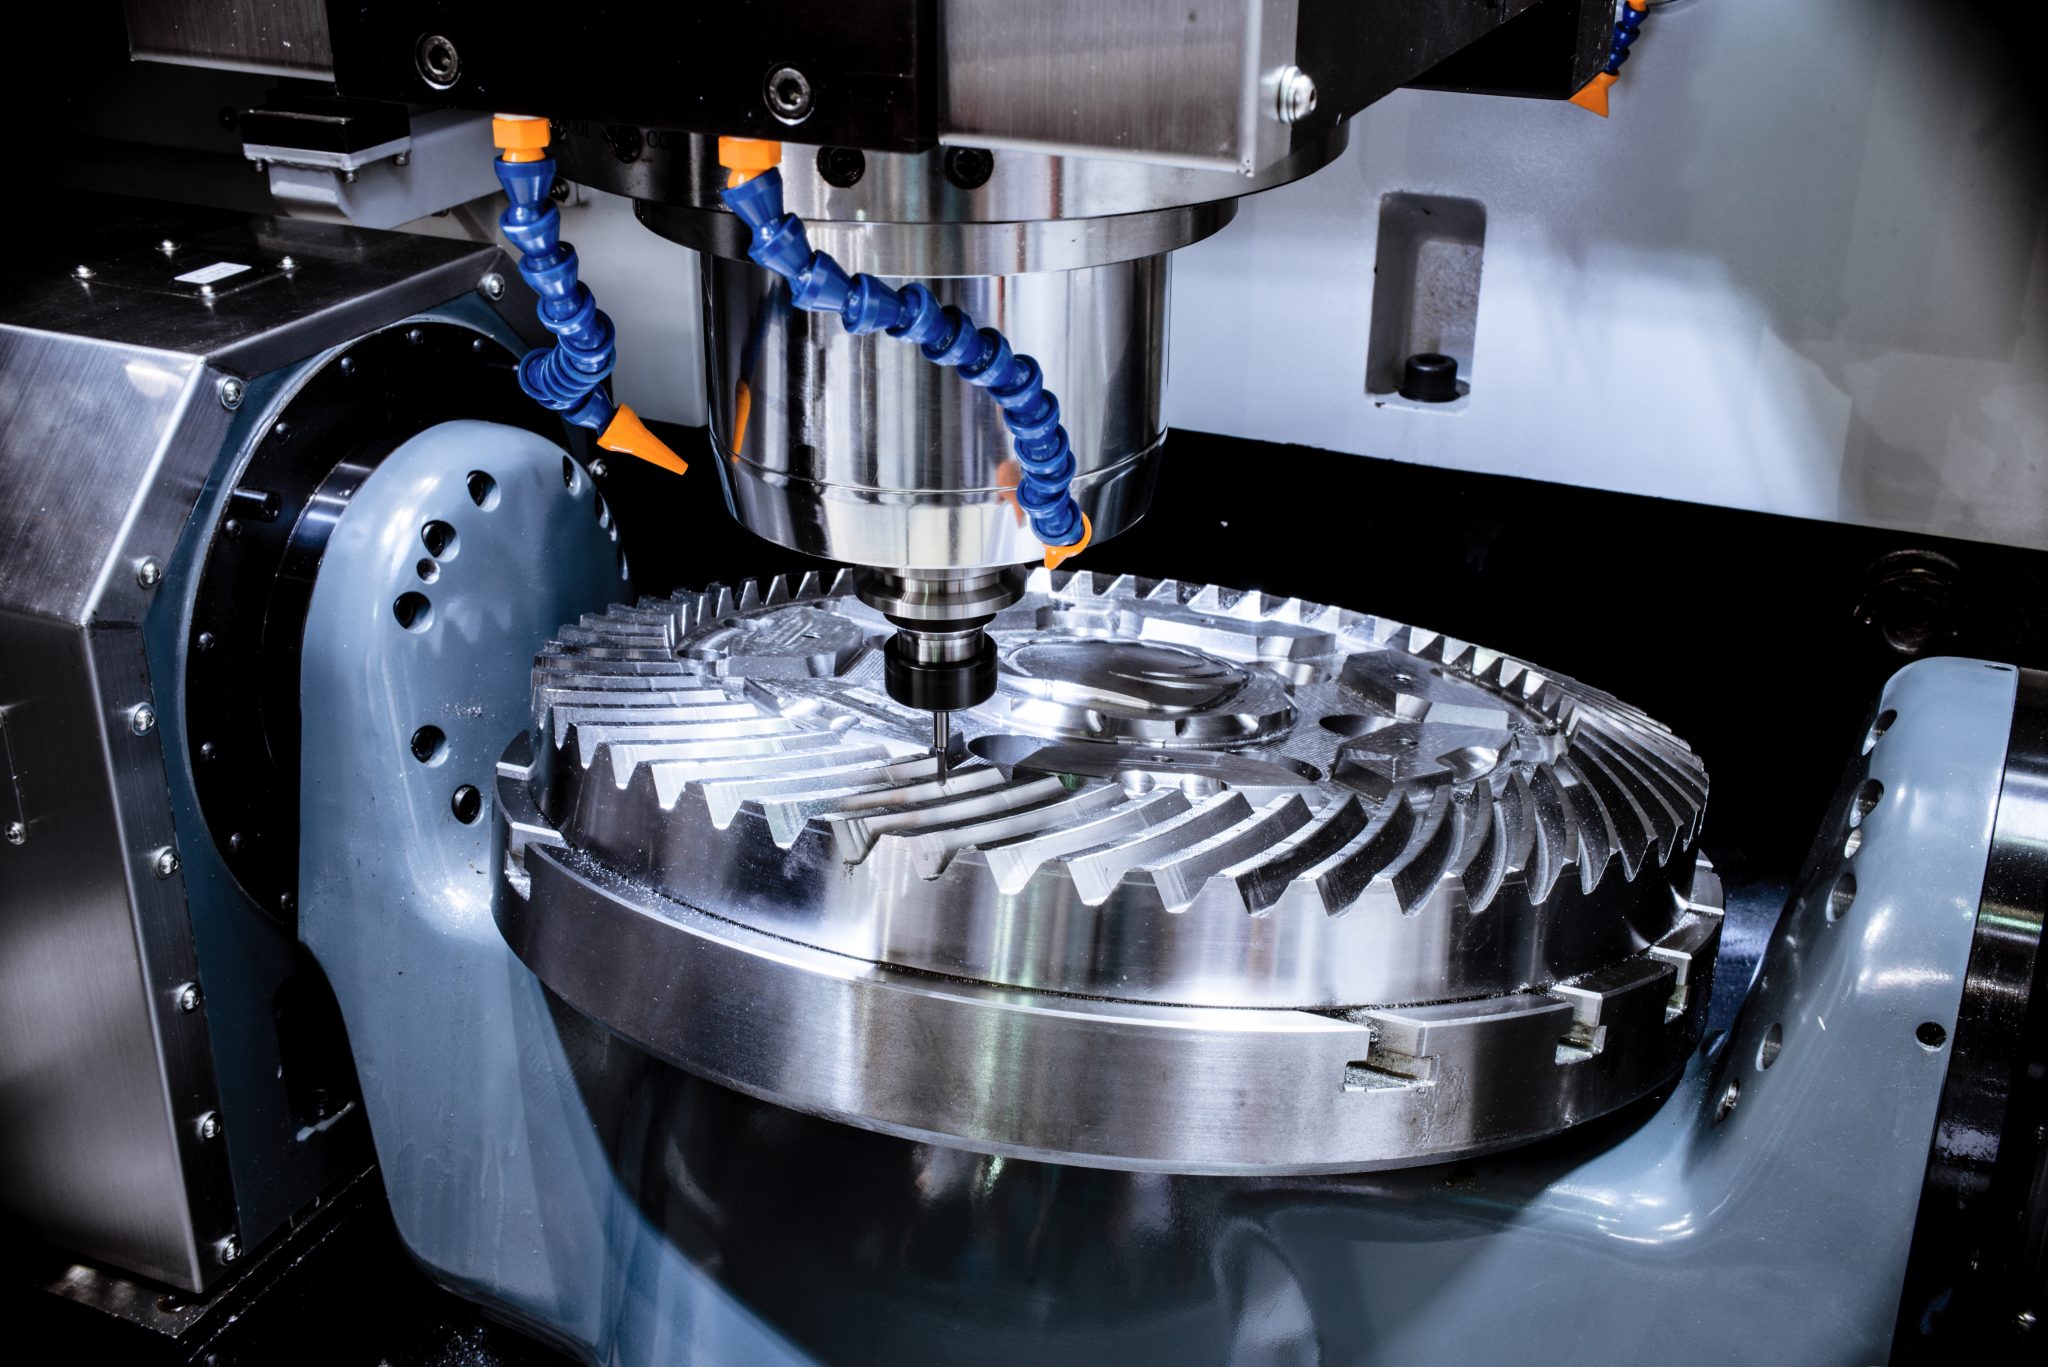
Multi-axis CNC machines — typically referring to 4-axis or 5-axis configurations — allow a cutting tool to approach a part from multiple angles without removing it from the machine.
Instead of repositioning the workpiece between operations, the machine itself rotates or tilts the tool (or the part, depending on configuration) to reach different faces and features in a single setup.
This capability is especially valuable for parts with complex geometry — angled holes, curved surfaces, or features on multiple faces — that would otherwise require several separate operations.
The shift from multiple setups to a single, continuous operation through multi-axis CNC machining reduces the cumulative error that comes from repositioning, while also cutting down on the total time a part spends in production.
Where This Capability Matters Most
Not every part benefits equally from multi-axis capability — a simple, flat component might be just as efficient to produce on a standard 3-axis machine.
The advantage becomes clear with parts that have complex, three-dimensional geometry: drilling components with angled ports, housings with features on several faces, or parts requiring tight tolerances across multiple planes.
In these cases, consolidating operations into fewer setups doesn’t just save time — it directly improves the consistency and accuracy of the finished part.
Precision Requirements in Field Equipment
Components used in drilling, mining, and geotechnical applications often face demanding operating conditions — high stress, vibration, and exposure to abrasive materials.
Parts that don’t meet precise tolerances can wear unevenly, fail prematurely, or simply not perform as reliably in the field.
Multi-axis machining supports the kind of tight, repeatable tolerances these applications require, since fewer setups mean less opportunity for the small deviations that can affect how a part performs under load.
Materials used in these applications add another layer of complexity. Hardened steels and other wear-resistant alloys, common in drilling and mining components, can behave unpredictably if cutting parameters aren’t matched to the material’s specific properties.
Combining the right material expertise with multi-axis capability allows a shop to hold tight tolerances even on parts made from materials that are notoriously difficult to machine consistently.
Efficiency Gains Beyond Precision
While accuracy is the primary advantage, multi-axis machining also affects production efficiency more broadly. Fewer setups mean less non-cutting time — the periods where a machine sits idle while a part is repositioned, re-fixtured, and re-verified.
For manufacturers producing parts at volume, this efficiency can meaningfully affect lead times without sacrificing the quality standards required for critical components.
What to Look for in a Machining Partner
Not every shop has invested in multi-axis equipment, and even among those that have, experience programming and operating these machines varies significantly.
A few things are worth asking about when evaluating a potential partner: What multi-axis capabilities does the shop actually have in-house, versus outsourced? What’s their experience with the specific materials and tolerances a project requires? Can they provide documentation of past work with similar part geometries?
Production volume flexibility is worth confirming as well. Some shops are set up well for prototype or low-volume work but struggle to scale efficiently, while others are optimized for high-volume runs but less agile with smaller, custom orders.
A partner capable of handling both ends of that spectrum offers more flexibility as a project’s needs evolve from initial development through full production.
A shop with decades of experience producing complex metal components tends to bring a deeper understanding of how to sequence operations efficiently, not just the equipment to execute them.
Built for Reliability in the Field
For companies producing equipment that has to perform consistently under demanding field conditions, the manufacturing process behind each component matters just as much as the material it’s made from.
Reducing setups, minimizing handling, and holding tight tolerances throughout production all contribute to parts that hold up where it counts — in the field, under load, over the long term.
Conclusion
Not every component needs multi-axis machining, but for parts with complex geometry or tight tolerance requirements, it’s often the difference between a part that meets spec reliably and one that requires rework.
A conversation with an experienced manufacturing partner is the clearest way to determine which approach fits a specific part’s requirements.


